Point a camera and a laser at your part, and our software turns the light that comes back into a 3D map of its surface, with the roughness numbers your drawing asks for. The bench surface profiler that captures it is built from catalogue optics and made to your order. Software-defined interferometric metrology.
Partnership: We are working with the P-DHM Yip Lab at the University of Toronto, under an LOI. We solved their depth-and-surface study bounty with our software and produced a result well beyond the open-source default path. Spin the 3D mesh yourself and read how it was made.
For developers
Bring your own camera. We bring the math.
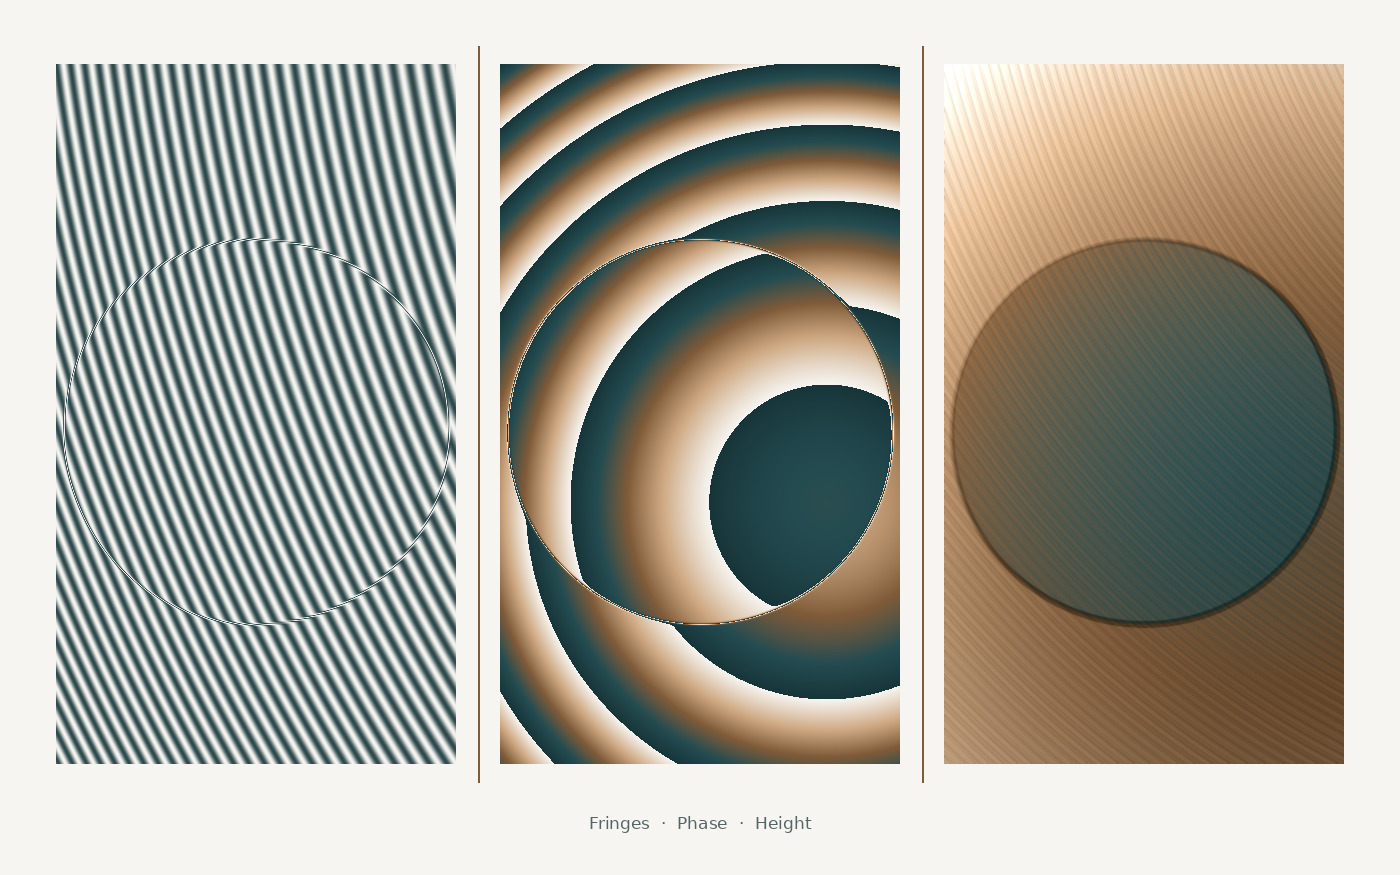
From fringes, to phase, to a finished height map.
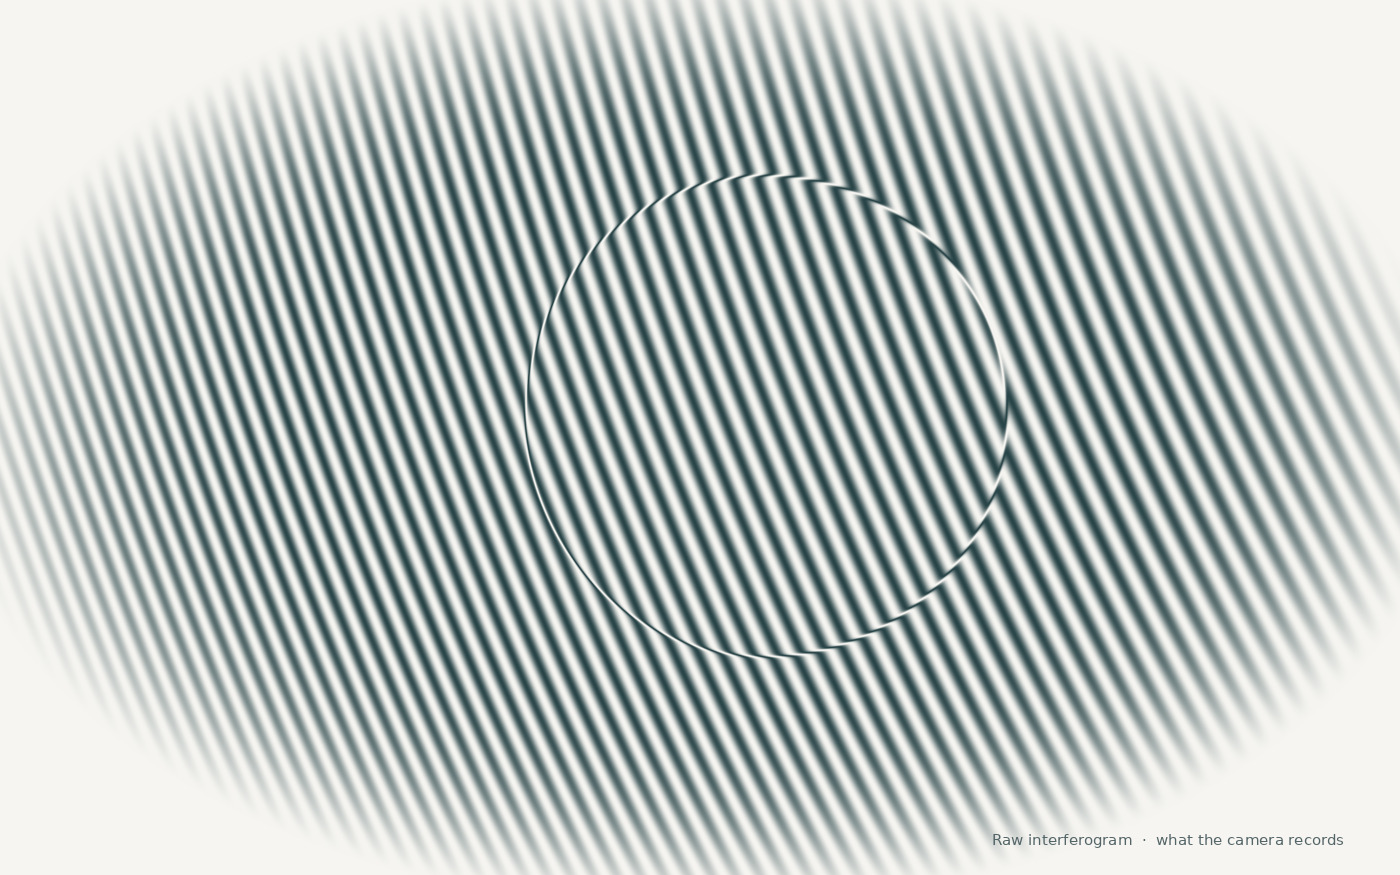
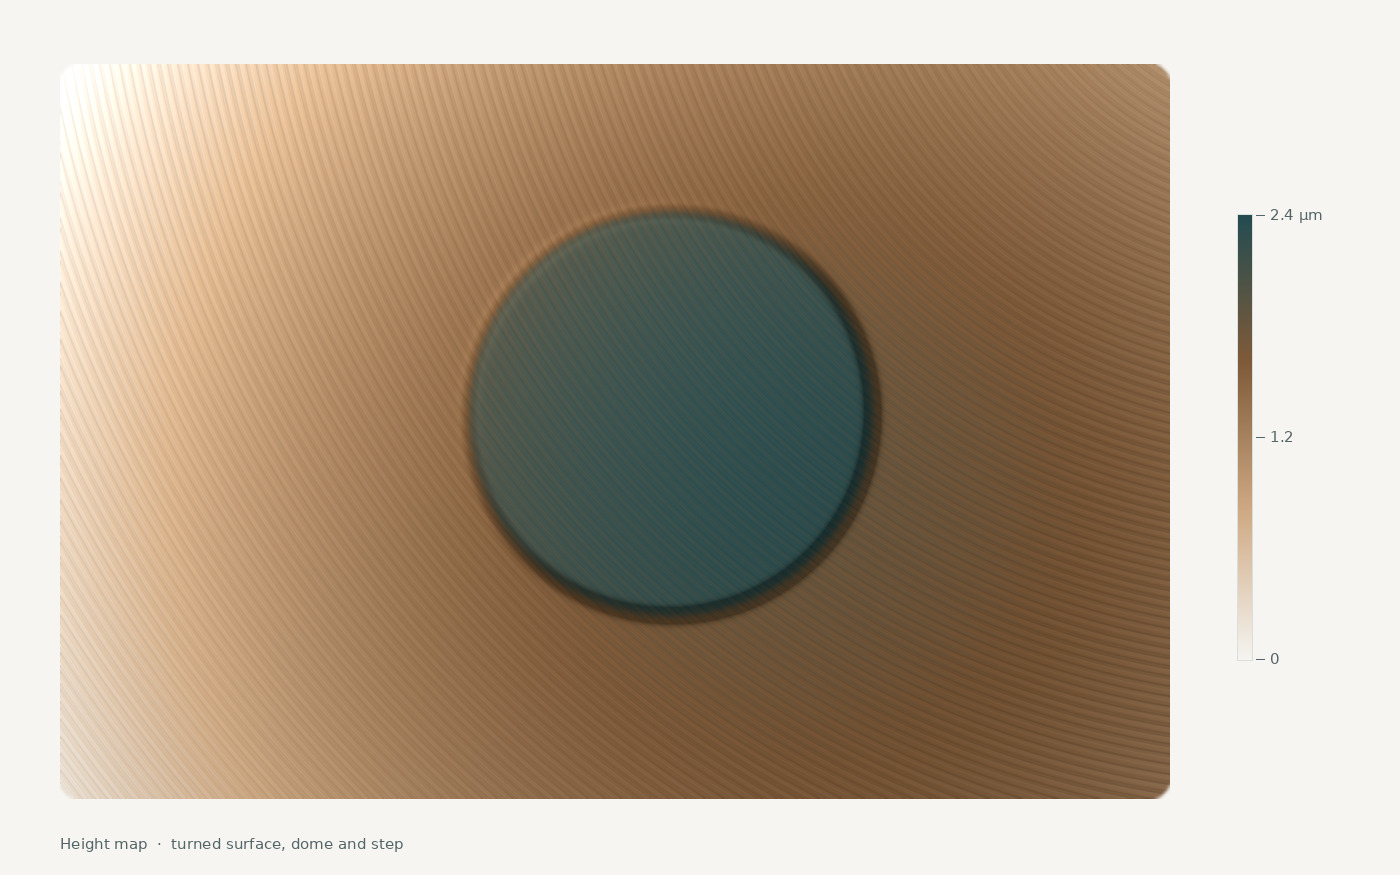
Send the hosted service a raw picture from an interferometer, a holographic microscope or your own rig, along with the laser wavelength, the camera pixel size and the distance to the part. Back come the amplitude, the phase and a height map, with a record of exactly how they were computed. The same software runs inside the instrument.
Two seats, simply priced. Lab is $150 a month and Engineering is $600 a month, with fifty and three hundred measurements included. Each one beyond that is $5.
A second measuring station beside the instrument you already trust, there for the checks that wait in its queue.
What the camera sees.What you get.
What comes back, every time
A 3D height map of the surface, as a file you can open and a picture you can share.
Roughness numbers in the standards your drawings already speak: Sa, Sq, Ra, Rq and the rest.
A computation record: the exact input, settings and software version, so anyone on your team can check it later.
A clear pass or fail against the limit you set before anyone looked at the data.
Where it fits
Height, shape and finish across a field from a few millimetres to a few centimetres, resolved to well under a micrometre.
Smooth and machined surfaces. For anything rougher than about 0.16 µm, there is a second-wavelength option.
Research labs and industrial QA.
Calibration profile
Calibrate the software to your rig.
Send up to twenty frames from your setup, along with the reference you measure against today. We fit a calibration profile to your optics (wavelength, pixel pitch, distance and aberrations) and compare the result with your reference against an acceptance limit we agree before we begin. The report comes back within ten business days. It is complimentary.
Just five short questions, and we follow up by email for the optical details. Or write to us at hello@apertureapi.com.
The instrument
A surface profiler that fits on your desk.
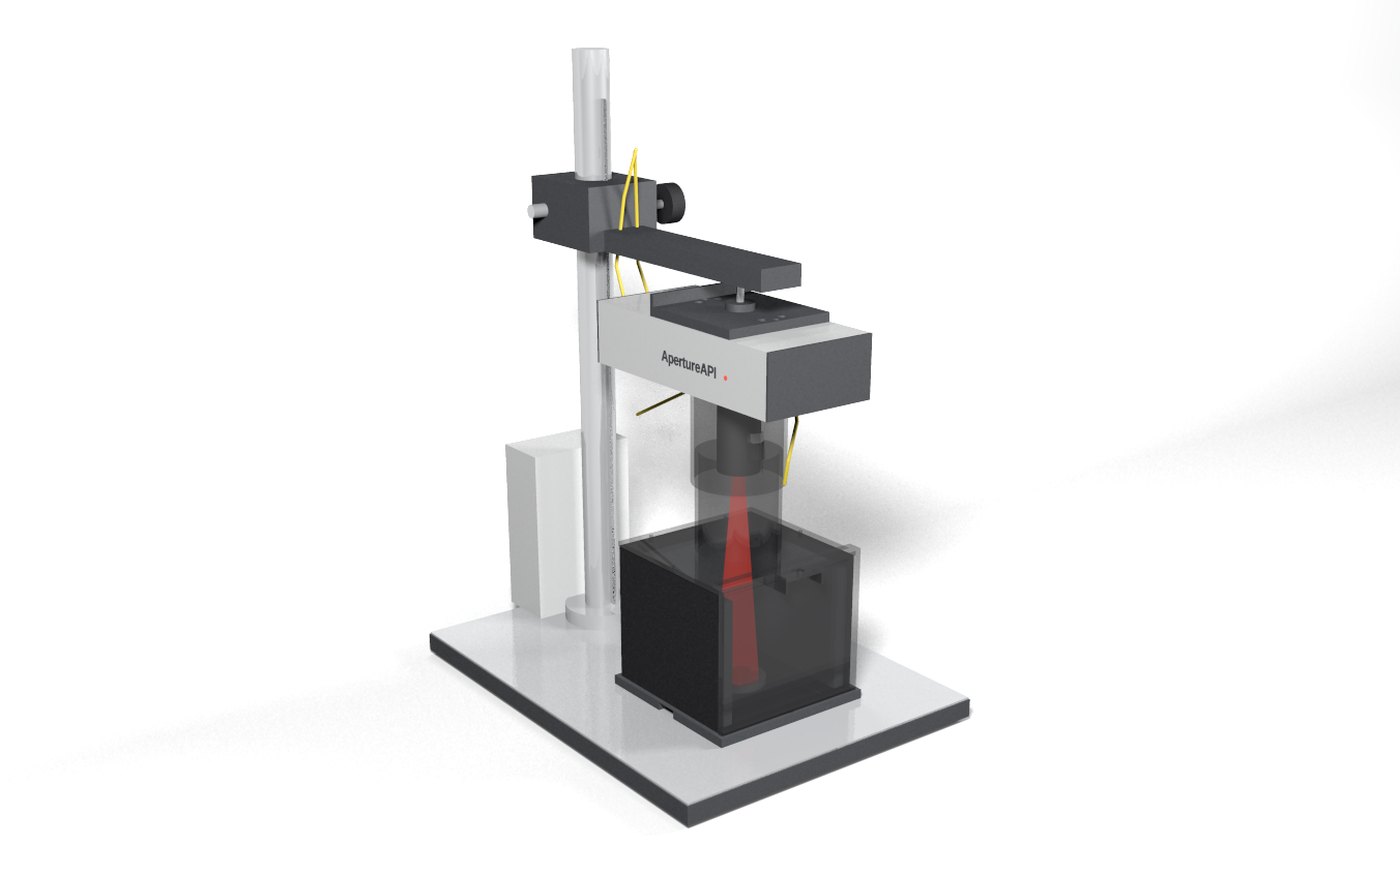
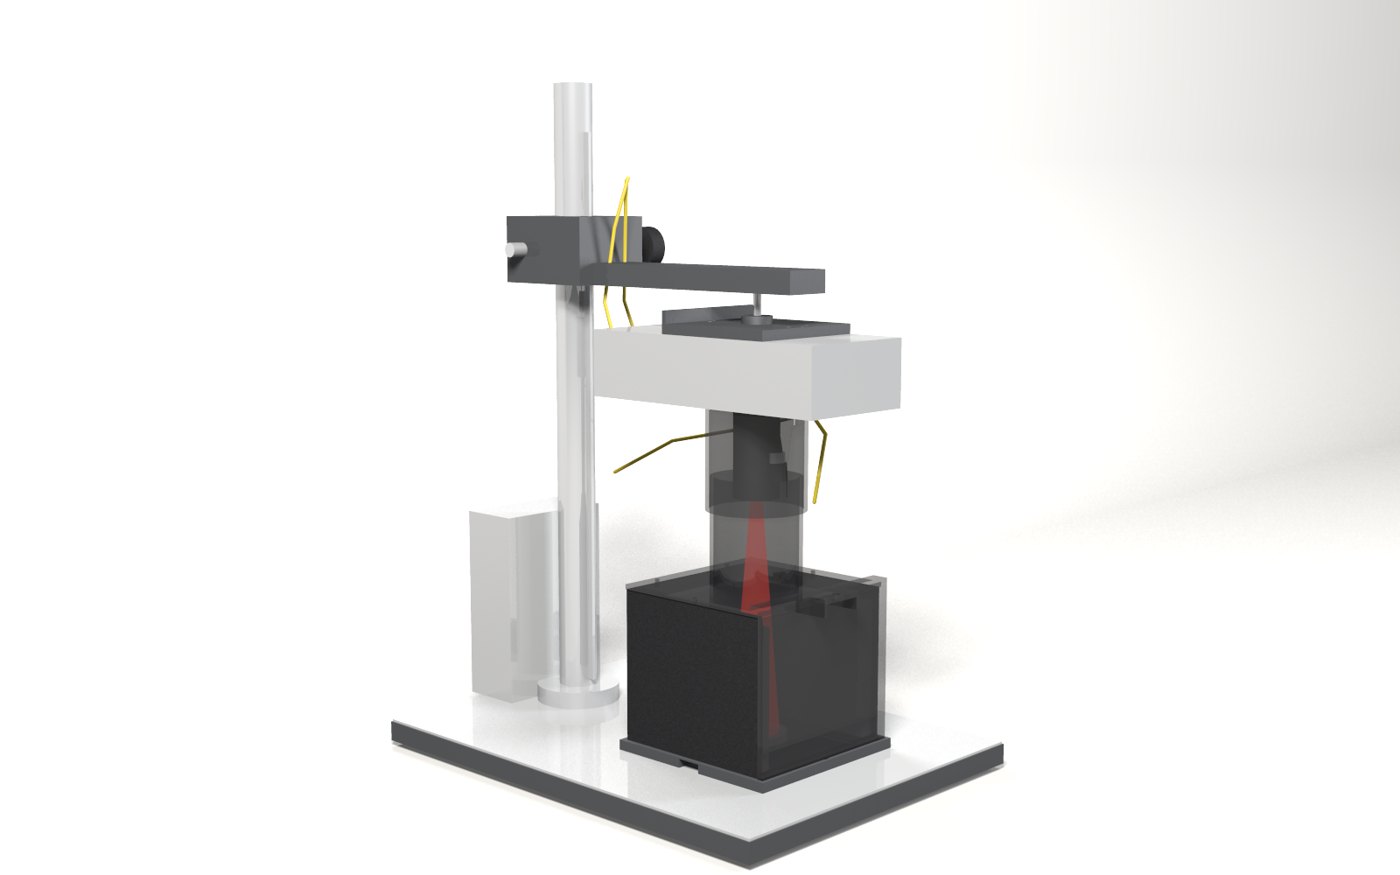
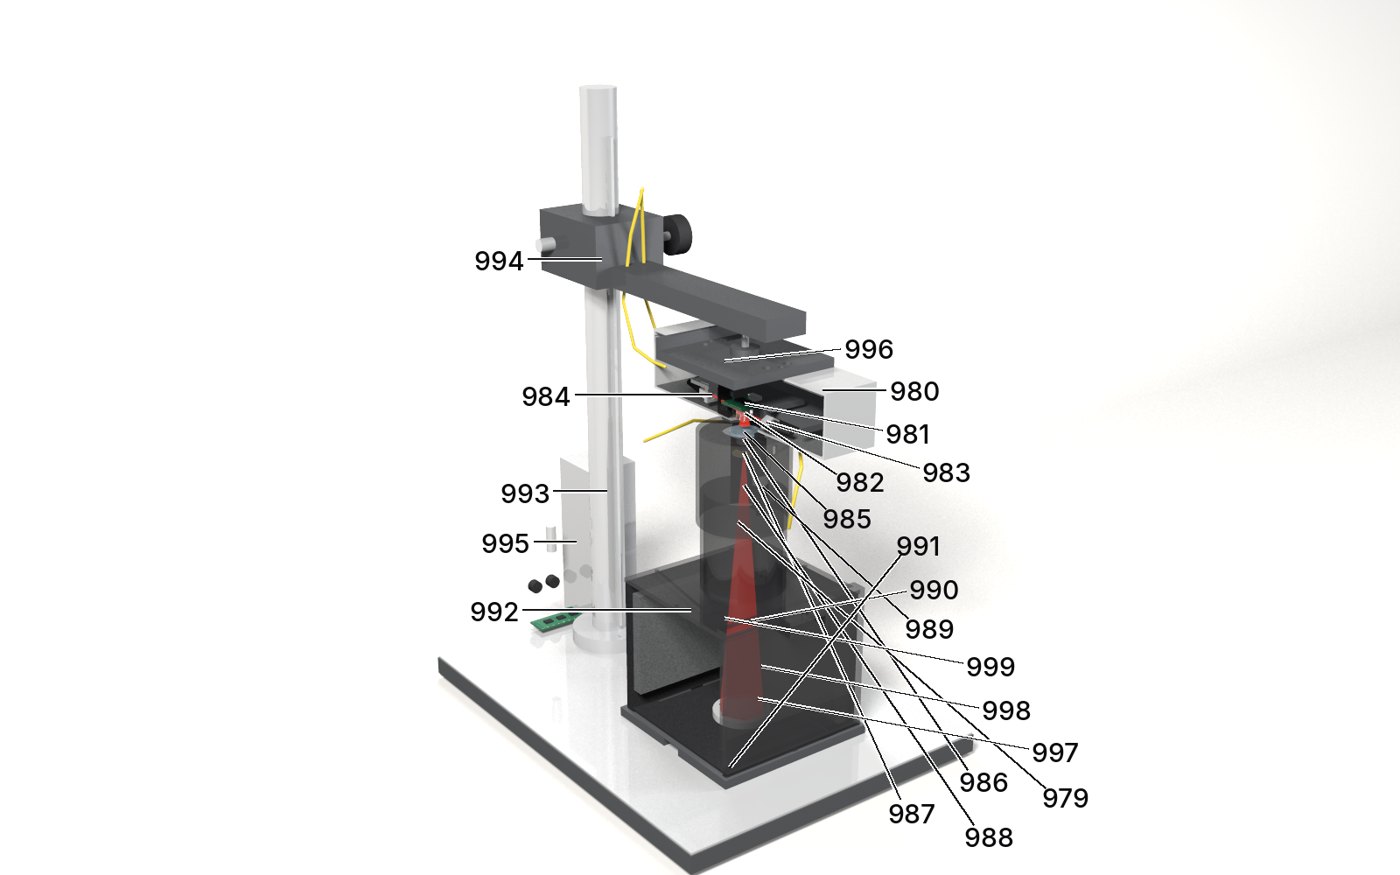
A sealed measurement head (H1) on a desk stand (D1). One camera, one laser, one measurement at a time: a column, a sliding head and a 150 × 150 mm table behind a lift-off front door, about the size of a small drill press.
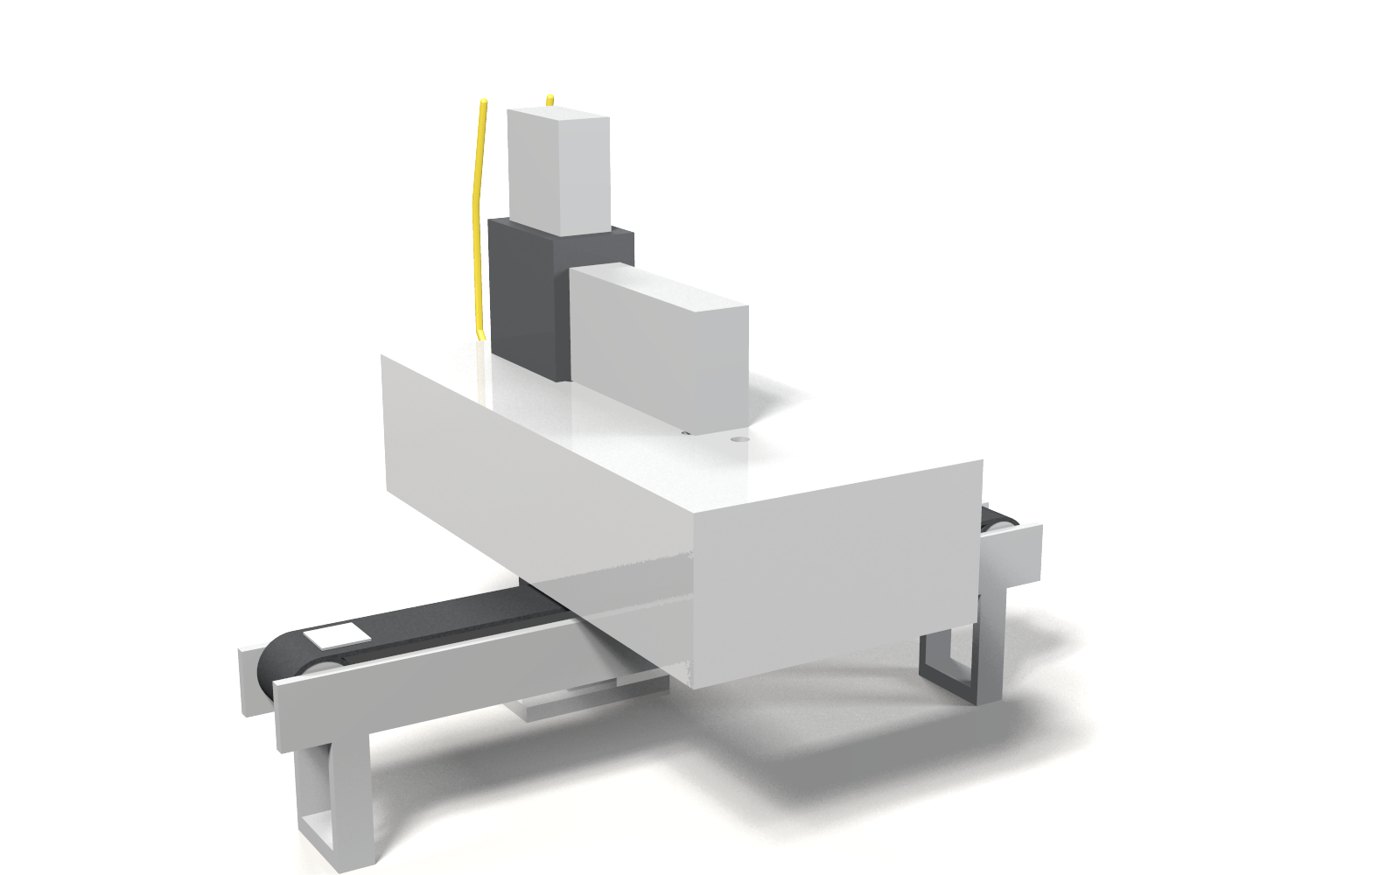
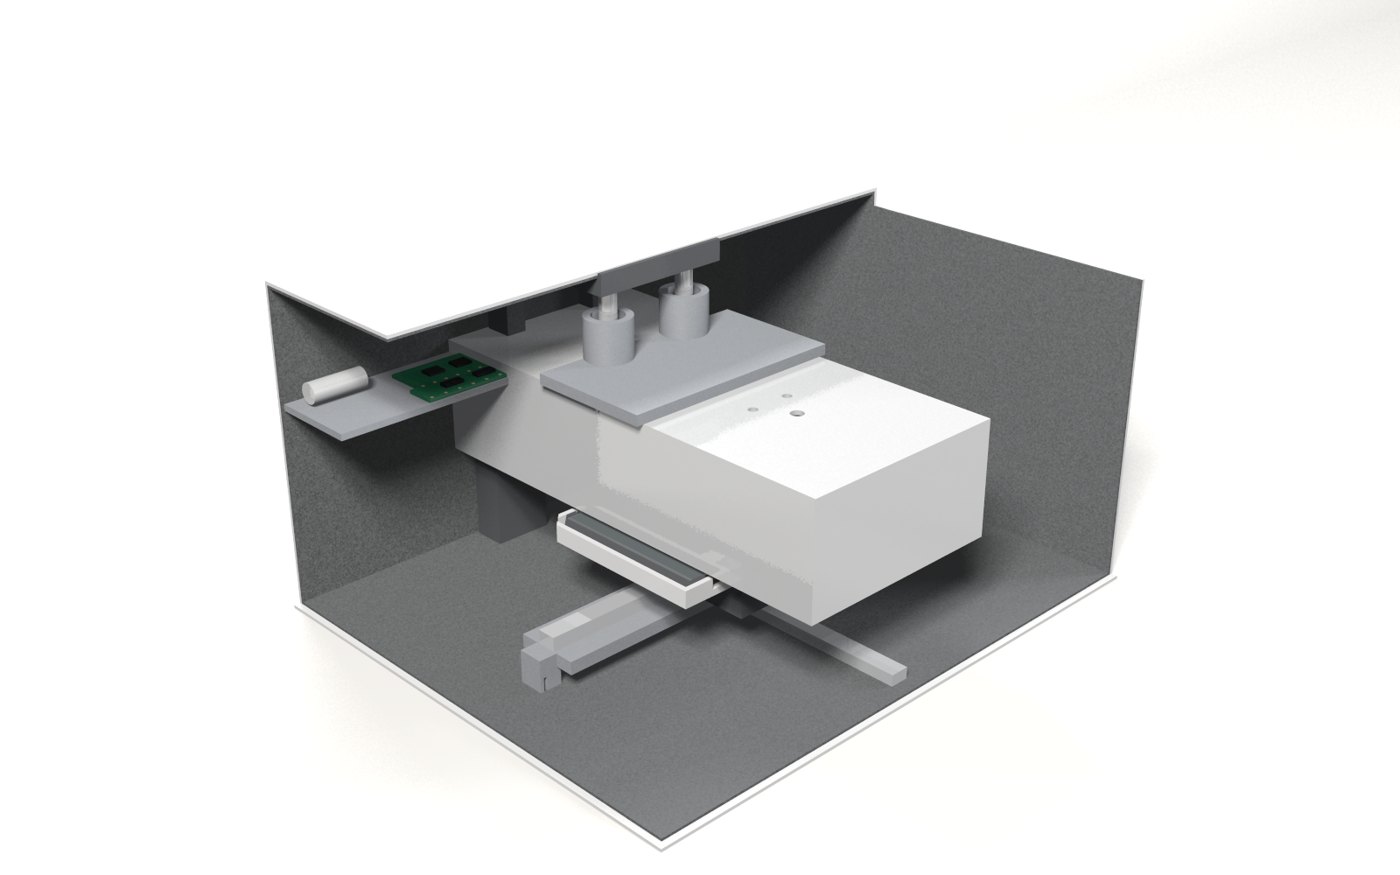
H1 on the D1 bench standH1 cutaway: optical path and interlockH1 on the B1 belt flange, inlineH1 over the T1 parts tray
01 / BENCH SURFACE PROFILER
H1 head on the D1 stand
$12,900 · second-wavelength option +$2,400
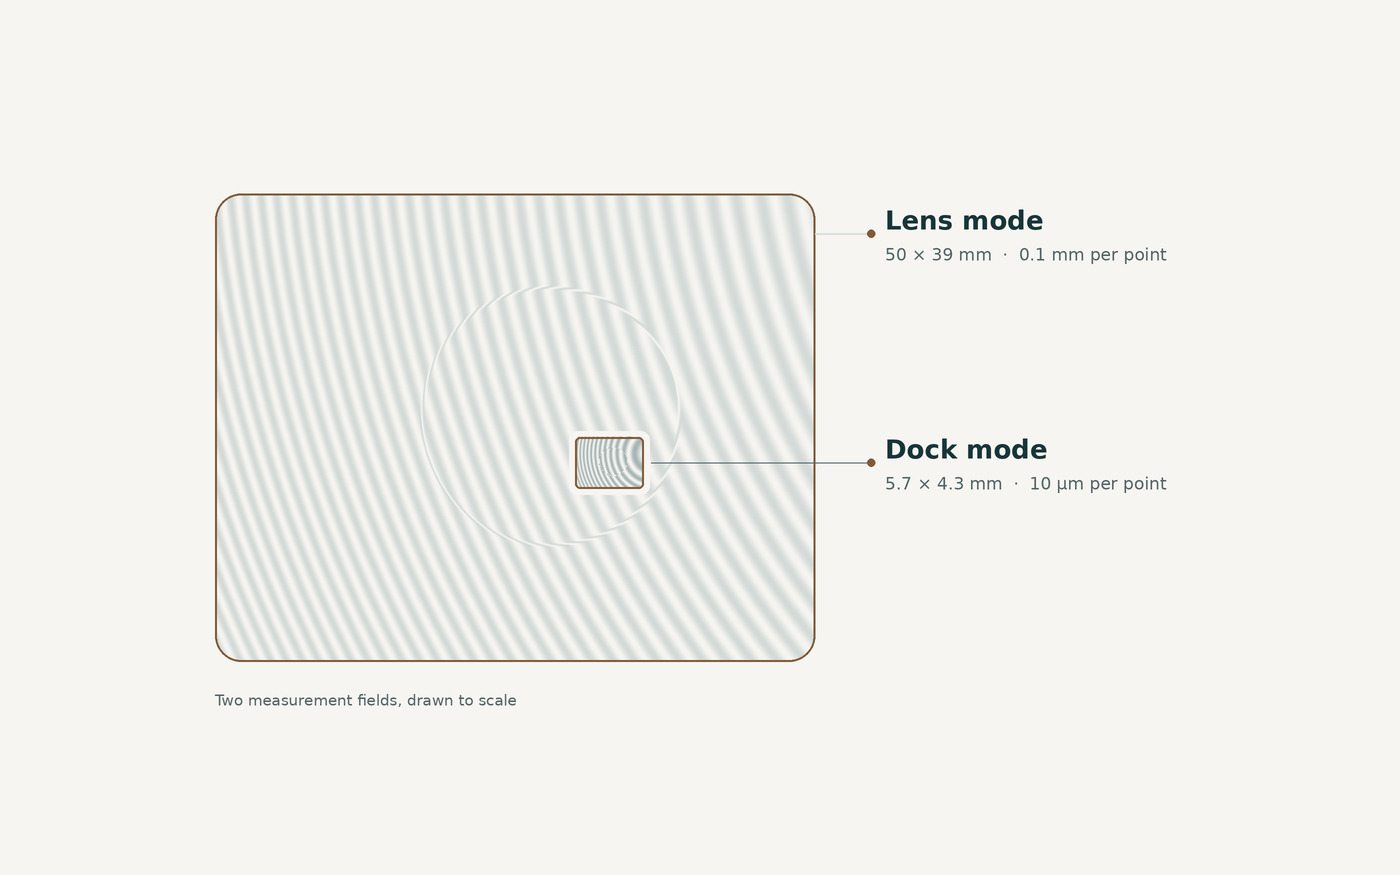
Lens mode. Maps matte, machined, printed, anodised and ceramic parts: a field of about 50 × 39 mm, a point every 0.1 mm.
Dock mode. A dock clips under the head for wafers, optics and flats: 5.7 × 4.3 mm per shot, a point every 10 µm, height resolved well under a micrometre.
Room light. Works in room light and window daylight, with the shroud and door seated.
Class 1 laser. The measuring zone is closed on four sides; the laser runs only with the door and back wall seated and the nose or dock in place. Open the door and the beam is off. A robot can lift the door between captures.
Included. Software, commissioning and ninety days of training and support.
02 / PURPOSE-BUILT
Shaped around your part
Included with every order
Sample beam width. Sized to your part and field.
Emitter colour. Laser wavelength chosen for your surfaces; a second wavelength for stepped and rougher parts.
Focal point. Set for your working distance and part height.
Mount. The same head on the D1 bench stand, the B1 belt flange for inline inspection, or the T1 tray for batches of parts.
Built from parts you can buy. Catalogue optics and electronics, a bought or printed enclosure, no custom machining. Parts lists and drawings ship with the unit.
Two fields, one head.
Six acceptance tests, in the open
Each test is written before it is run, and each sheet is published as it is completed.
Test
What is measured
Compared against
Pass if
1. Light source and dock
Fringe visibility; ghost signal after background removal
Flat mirror
Visibility at least 0.5; ghost at or below −20 dB
2. Lens-mode physics
Coherence over a path scan, light balance, ghost residual, shape map of a matte tile
Path scan and a matte tile
Coherence revival within ±32 mm; ghost at most 10 % of the object
3. Customer set-up, timed
Time for a new operator to run the flat capture and scale grid
Stopwatch; flat and scale grid
60 min or less
4. Room light
Fringe contrast at 500 and 2,000 lux with the walls and door seated
Contrast with room light off
Contrast loss at most 1 %
5. Stand and laser interlock
Head sag, re-seat repeatability, interlock chain
Each door and wall opened in turn; each switch tried for a tool-free bypass
Sag at most 1 mm; laser never on with any door or wall open; no switch bypassable without tools
6. Step standard and repeat readings
Step height and repeated measurements on a customer part
Step standard
Within the uncertainty agreed with the customer
How we prove it
You set the bar. Then we measure.
Every evaluation compares one set-up with a reference you already trust, against a limit agreed in advance. Software checks and physical measurements are always reported separately.
Agree
Together we write down the part, the area, the result you need, the time per part and the reference, before a single picture is taken.
Measure
We record the conditions and the settings, compare with the reference, repeat the measurement, and go looking for the cases where it fails.
Decide
You see the results, the full cost of a unit and how it fits your workflow, judged against the limit agreed in step one.
Prices and how to buy
Three steps, and no surprises.
Begin with a calibration profile for your own rig. The application study then builds and proves the set-up with a signed report, and every dollar of it is credited toward the instrument. Units are built to order on a deposit.
How it unfolds
Calibration profile. Up to twenty of your frames, one reference, one acceptance limit agreed first, report in ten business days. Complimentary.
Application study, $4,800 in two payments. $2,400 on signing: we build and bench-test the set-up for your part. $2,400 at the signed report, with the acceptance criteria fixed before the first picture. Credited in full to the instrument.
The instrument. The bench surface profiler $12,900; second-wavelength option +$2,400. Software, commissioning and ninety days of training and support included. Half on order, half on delivery.
Development partnerships. Built around your own camera, or built around you: $10,000 software, $25,000 hardware.
What the study report includes
Raw and processed data with the settings and the reference record.
The comparison with your reference, repeated readings, a map of where it fails, and the uncertainty for your task.
A demonstration: install, check the reference, load a part, read the output.
The parts list for your unit.
A written recommendation: buy, repeat one bounded test, or stop.
Research and industrial QA
A second station for the queue, beside the instrument you already trust.
Built to order
Half on order, half on delivery. Lead time is stated on the order.
Software seats
Lab $150 a month. Engineering $600 a month. $5 per extra measurement.
Bring one part.
Tell us what the part is, what you need to measure on it, and where the measurement has to fit in your day. We will take it from there.